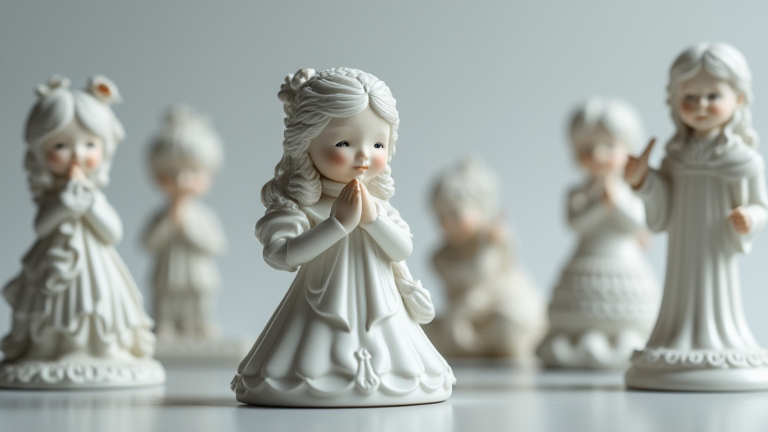
TL;DR: 3D scanning and printing now allow museums and collectors to create high-fidelity porcelain figurine replicas with sub-0.05 mm accuracy, preserving intricate lace-like details and glaze undercuts that were previously impossible to replicate. The latest resin printers with ceramic-filled photopolymers can produce fireable “green” bodies that shrink predictably by 18–22%, enabling true porcelain composition (kaolin + feldspar) in final firing.
From Fragile Antique to Digital Twin: The Scanning Revolution
The latest structured-light 3D scanners (e.g., Artec Space Spider, EinScan Pro HD) capture figurine surfaces at 0.03 mm resolution, using blue LED light that doesn’t heat or damage delicate glazes. For translucent pieces, multi-axis turntables with 360° polarimetric imaging map subsurface scattering—critical for replicating the milky glow of Qing dynasty famille rose. New handheld LiDAR hybrids (like the Revopoint POP 3) now offer 0.02 mm repeatability for under $2,000, down from $50k systems a decade ago. Specs that matter: 16-bit depth maps, 10 fps capture, and automatic mesh cleanup that removes support-strut shadows without touching the figurine’s original surface.
If you want to dig deeper, check out our guide on Here are a few options, all under 70 characters:
1. **Tech .
Ceramic-Filled Resins: The Printing Breakthrough
Traditional FDM printers failed at porcelain because layer lines destroyed the smooth ivory finish. Enter digital light processing (DLP) printers with ceramic slurries—e.g., Tethon 3D’s Bison 1000 or Lithoz’s LCM systems—that mix 45–55 vol% alumina/silica particles in a photopolymer binder. After printing, parts undergo debinding (400°C) and sintering (1250–1350°C) to achieve true porcelain density (2.4 g/cm³). New “lost-wax hybrid” workflows print a wax-positive figurine, then invest it in plaster for slip-casting the final porcelain—this preserves the original’s hollow weight and ring tone. Key spec: layer thickness of 25–50 µm, with a green-strength modulus of 12 MPa to prevent sagging of raised arms or petticoats during handling.
Industry Impact: Restoration and Mass Customization
Major porcelain houses (Meissen, Lladró, Royal Copenhagen) now scan archival molds dating to the 1700s, creating digital catalogs for on-demand reproductions—cutting lead time from 6 months to 3 days. For damaged figurines, 3D-printed “surgical grafts” of missing fingers, flowers, or bases are glued with UV-curing ceramic adhesive, then re-fired to blend the join line invisibly. The art market sees a new niche: “scan-to-own” services where collectors pay $300–$800 for a master scan of their heirloom, then print limited edition resin-porcelain hybrids (not fireable but UV-stable) for garden display. However, ethical debates arise: museums limit public scans to prevent counterfeit “authentic” pieces from flooding auctions, as optical scans capture even craquelure and brushstroke micro-relief—making forgery detection harder without destructive testing.
FAQ
Q: Can 3D-printed porcelain figurines be fired in a standard home kiln?
A: No—ceramic-filled resins require industrial debinding ovens with controlled atmosphere and sintering furnaces reaching 1350°C. Home kilns (max 1200°C) will cause warping or blistering. Use a service like Shapeways or Sculpteo for fireable parts.
Q: What is the maximum size of a figurine that current printers handle without support structures?
A: Most DLP ceramic printers have a build volume of 192×120×200 mm. Larger figurines (over 25 cm) must be sliced into 3–5 interlocking pieces with internal pegs, then joined with ceramic slip and re-fired—this adds visible seam lines unless polished post-sintering.
Q: How do
Leave a Reply